Wholesale 1000 Liter Heavy Duty IBC Tank Container with Pallet for Liquid Storage Manufacturer, Factories
Product Description
Product Introduction
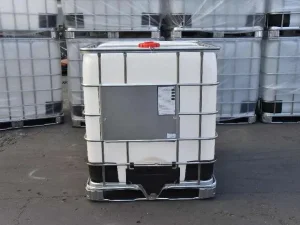
Construction & Materials
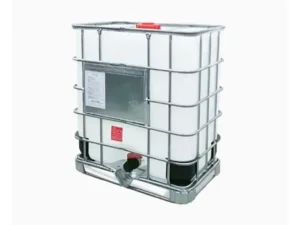
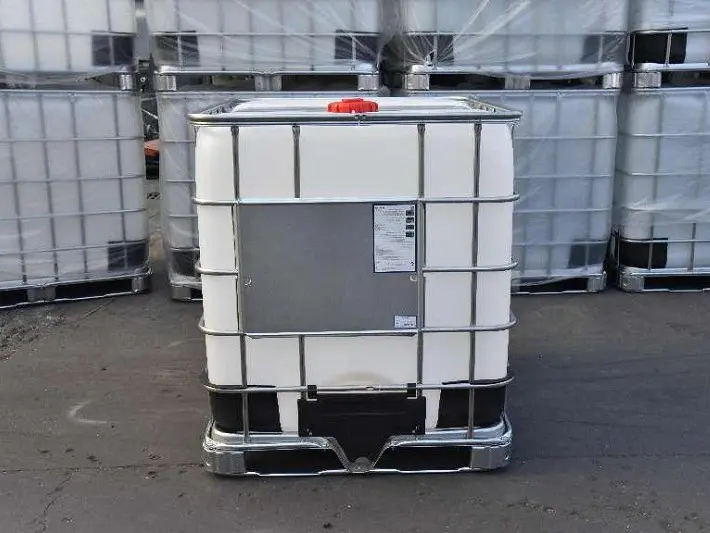
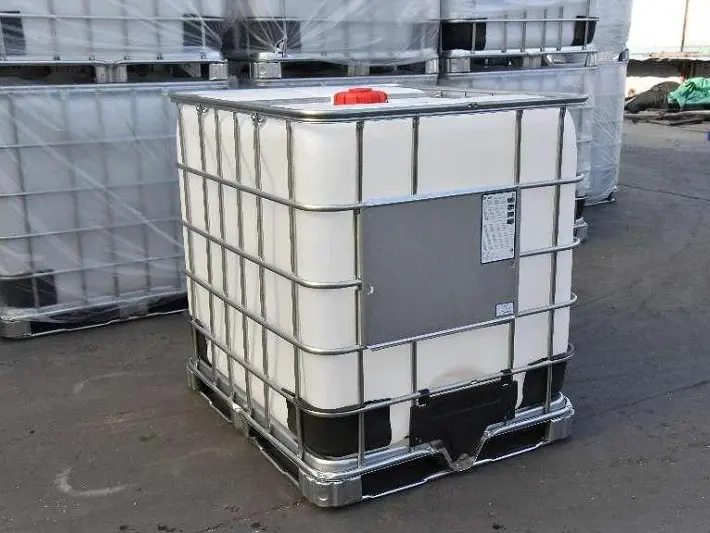
Inner Tank: Manufactured from high-density polyethylene (HDPE) using rotational molding or blow-molding, ensuring a seamless, leak-proof design. The material is FDA-compliant for food-grade applications and resistant to a wide range of acids, alkalis, and chemicals.
Outer Cage: Constructed from hot-dip galvanized steel tubes (typically 40mm x 40mm), providing strong structural support and corrosion resistance.
Pallet Base: A heavy-duty steel pallet (standard size 1200mm x 1000mm) with four-way forklift entry for safe and stable handling.
Technical Specifications
Capacity: 1000 liters (264 gallons).
Dimensions: Approximately 1200mm (L) x 1000mm (W) x 1150mm-1200mm (H).
Weight: Tare weight ~65-75 kg; maximum gross weight (filled) of 1200-1250 kg.
Temperature Range: Can safely withstand contents from -40°C to 70°C without material degradation or leakage.
Key Features
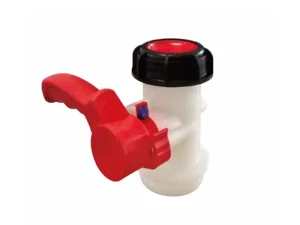
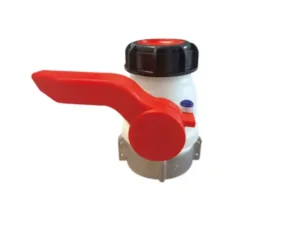
Bottom Discharge Valve: Equipped with a 2-inch standard ball or butterfly valve at the bottom, allowing fast, controlled, and complete drainage while minimizing residue.
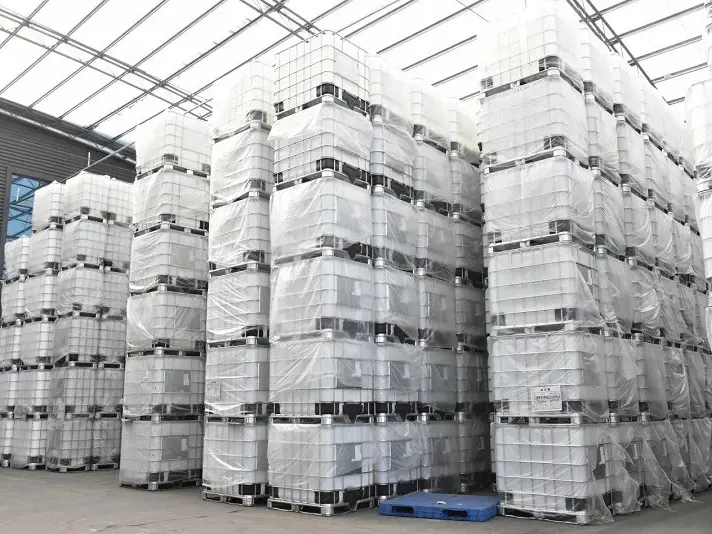
Stackability: Designed to be stacked up to 3 units high when fully loaded, optimizing warehouse and transport space.
Reusability & Sustainability: Fully reusable and recyclable, reducing packaging waste and total cost of ownership over multiple cycles.
Performance & Safety
Load Capacity: The steel cage and pallet are engineered to support dynamic loads during transport and static loads in stacked storage.
Compliance: Can be manufactured to meet UN certification (e.g., UN 31HA1/Y) for the transport of hazardous and non-hazardous liquids.
Safety: Seamless inner tank eliminates weak points, while the robust frame protects against impacts and accidental drops.
Applications
Suitable for storing and transporting chemicals, solvents, liquid fertilizers, food-grade liquids (oils, syrups), pharmaceuticals, and water.
Widely used in agriculture, manufacturing, food & beverage, logistics, and water treatment sectors.
Operational Advantages
Space Efficiency: Its cubic design allows up to 35% more efficient use of storage and shipping space compared to traditional round drums.
Low Maintenance: Requires no regular maintenance or cleaning under normal use, and the smooth inner surface allows easy cleaning when needed.
Cost Savings: Reduces handling, storage, and disposal costs due to its reusability and efficient footprint.
Frequently Asked Questions (FAQ)
Q1: What materials are used to construct the tank and frame?
The inner tank is made from FDA-compliant high-density polyethylene (HDPE), the outer cage consists of hot-dip galvanized steel tubes, and the base features a heavy-duty steel pallet.
Q2: What is the total capacity and dimensions of the unit?
The container has a capacity of 1000 liters (264 gallons) with approximate dimensions of 1200mm (L) x 1000mm (W) x 1150mm-1200mm (H).
Q3: What temperature range can this container safely withstand?
It can safely hold contents within a temperature range of -40°C to 70°C without experiencing material degradation or leakage.
Q4: How high can these containers be stacked when fully loaded?
The structural design allows them to be stacked up to 3 units high when fully loaded to optimize warehouse and transport space.
Q5: Is this container certified for transporting hazardous materials?
Yes, it can be manufactured to meet UN certifications (such as UN 31HA1/Y) for transporting both hazardous and non-hazardous liquids.
Q6: How does this design improve operational efficiency over traditional drums?
Its cubic design utilizes storage and shipping space up to 35% more efficiently than round drums, while the 2-inch bottom discharge valve ensures fast and complete drainage.