Featured Industrial Containment & Valve Solutions
Factory-direct fluid handling components and bulk liquid storage solutions manufactured under ISO 9001:2015 quality standards.
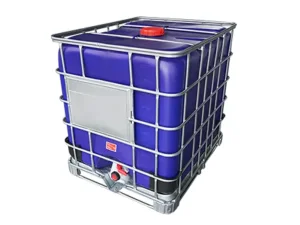
Industrial Liquid Containment Architecture & Strategic Sourcing
In modern globalized chemical processing, pharmaceutical manufacturing, and agricultural bulk distribution, selecting an optimal wholesale industrial liquid storage tank manufacturer goes beyond standard purchasing—it represents a mission-critical risk management strategy. Industrial Intermediate Bulk Containers (IBCs), high-density drums, and modular containment systems form the physical backbone of global fluid logistics. As global regulatory bodies enforce stricter transport safety standardizations (such as UN dangerous goods codes, ADR, and IMDG regulations), industrial liquid storage systems must demonstrate structural integrity under extreme thermal dynamic stresses, hydrostatic pressures, and aggressive chemical exposure.
An enterprise-grade liquid storage system requires zero-leak fluid mechanics, high environmental stress crack resistance (ESCR), and modular interoperability. Whether storing volatile organic solvents, corrosive mineral acids, high-viscosity food concentrates, or ultra-pure agricultural liquids, fluid containment vessels are expected to maintain chemical inertness while enabling rapid filling and discharge. As a leading manufacturer based in China's industrial manufacturing core, our engineering facilities integrate high-molecular-weight High-Density Polyethylene (HMW-HDPE) extrusion blow molding with automated robotic steel frame welding, setting a new benchmark for structural longevity and unit economics.
The Chinese Manufacturing Supply Chain Advantage in Bulk Packaging
The industrial hub of Linyi, Shandong, has evolved into global dominance in precision polymer engineering and industrial bulk container manufacturing. Sourcing industrial liquid storage tanks directly from audited Chinese manufacturing factories provides global procurement managers with unprecedented strategic advantages across cost optimization, custom tooling velocity, and end-to-end quality assurance.
Vertical Integration: From Polymer Resin to Completed Tote Assembly
Unlike regional assembly facilities that outsource individual components, top-tier Chinese manufacturing complexes operate complete backward-integrated supply chains. High-density polyethylene resin is sourced directly from petrochemical refineries, subjected to differential scanning calorimetry (DSC) melt-flow testing, and processed in multi-layer blow molding machines. Simultaneously, automated cold-roll steel forming mills produce hot-dip galvanized steel tubing for outer protective cages, while CNC tooling centers machine internal valve components down to a precision tolerance of 0.005 mm.
Custom OEM/ODM Tooling Capabilities
Global distributors frequently require custom modifications to match proprietary filling lines or specialized chemical transport specs. Chinese engineering teams excel in rapid prototype development, mold flow analysis, and low-cost tooling modifications. Whether developing fluorinated inner liners to prevent solvent permeation, engineering anti-sloshing internal baffles for marine transportation, or customizing color-coded breathable screw caps, direct factory partnerships reduce mold prototyping cycles from months to mere weeks.
Technical Compliance & Engineering Specification Matrix
When evaluating wholesale industrial liquid storage tank factories, technical procurement specialists must analyze key structural metrics to ensure operational compatibility and transport safety. Below is a comprehensive engineering comparison matrix across common industrial containment architectures:
| Performance Criteria | 1000L Composite IBC Tote (HDPE + Steel) | Stainless Steel IBC (SS304/SS316L) | 50L - 200L High-Density Plastic Drums |
|---|---|---|---|
| Primary Application | Bulk liquid chemicals, food syrups, oils, water | High-purity solvents, cosmetics, hot liquids (>90°C) | Small-batch chemicals, lubricants, liquid reagents |
| Tare Weight Efficiency | Optimal (~55-65 kg per 1000L payload) | Heavy (~140-180 kg per 1000L payload) | Moderate (~8-10 kg per 200L capacity) |
| Stacking Capability | 4-High Statically Loaded (1.9 Specific Gravity) | 6-High Statically Loaded | 3-High Palletized Stacking |
| Chemical Compatibility | Broad (Acids, Bases, Water-based Solutions) | Exceptional (Organic Solvents, Aromatic Hydrocarbons) | High (General industrial liquids, corrosive fluids) |
| UN Dangerous Goods Mark | UN 31HA1/Y Certified Options | UN 31A/Y Certified Options | UN 1H1/Y & 1H2/X Certified |
| Discharge Valve Configurations | Integrated DN50 / DN80 Butterfly or Ball Valves | Top/Bottom Flanged Ball Valves (SS316) | NPT/BSP Screw Bung Outlets |
| Unit Economics | Lowest cost per liter stored | High initial capital, long-term multi-use cycle | Low per-unit cost, higher handling labor |
Localized Application Scenarios & Industry Adaptations
Industrial liquid storage requirements vary greatly depending on local operating environments, regional chemical transport regulations, and specific vertical market demands. Professional storage tank manufacturers tailor structural density, valve seals, and UV protection to excel in localized operational environments:
Industry Trends: ESG Compliance, Smart IBCs & Circular Economy
The industrial liquid packaging sector is undergoing a profound technological evolution driven by corporate ESG commitments, carbon reduction mandates, and IoT digital supply chain visibility:
1. Closed-Loop Tote Reconditioning & Material Recyclability
Global chemical conglomerates are moving away from single-use IBC totes toward closed-loop reconditioning models. Modern composite IBCs are engineered for easy bottle replacement (rebottling) while preserving the heavy-duty galvanized steel outer cage for 10+ operational cycles. In addition, post-industrial HDPE bottle materials are 100% recyclable, feeding into secondary non-UN plastic pallet manufacturing to achieve zero-landfill targets.
2. IoT-Enabled "Smart IBC" Integration
Modern wholesale manufacturers now design IBC lids and caps featuring integrated ATEX-certified GPS tracking slots, ultrasonic liquid level sensors, and internal temperature monitors. This allows fleet managers to track real-time container position, monitor ambient temperature thresholds during chemical transit, and automate inventory reordering when tank levels drop below critical thresholds.
3. Lightweight High-Tensile Structural Materials
Innovations in structural geometry and high-tensile lightweight aluminum pallet bases allow up to a 12% reduction in overall tare weight without sacrificing static or dynamic load capacities. Reduced tare weight directly translates to lower fuel consumption and carbon emissions during long-distance intermodal freight shipping.
Frequently Asked Questions: Technical Procurement Guide
Direct answers from our engineering team to common procurement, compliance, and technical questions raised by global enterprise buyers:
Industrial Replacement Parts & Accessory Hardware
Maintain and upgrade your industrial container fleet with precision replacement accessories direct from our manufacturing lines.