Featured Industrial IBC Valves & Storage Components
Factory-direct wholesale equipment rigorously tested for structural integrity, chemical resistance, and zero-leak performance.
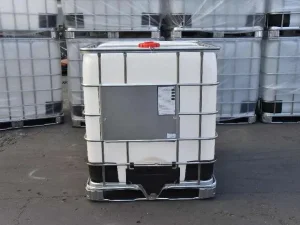
The Critical Role of IBC Valves in Global Bulk Liquid Logistics
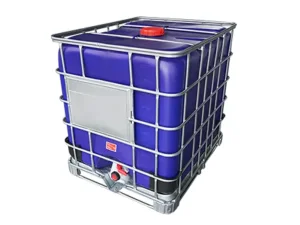
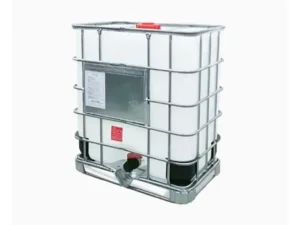
Intermediate Bulk Containers (IBC totes) represent the backbone of global chemical, food ingredient, and industrial liquid transportation. Within this supply chain, the discharge valve is the single most vital component governing fluid dynamics and environmental safety.
Zero-Tolerance Leak Prevention
Industrial chemicals and hazardous materials require absolute containment during multi-modal transit (sea, rail, and highway). A microscopic valve stem clearance defect can result in catastrophic environmental contamination, regulatory fines, and supply chain downtime. High-grade OEM valves guarantee leak-free operation up to 2.5 bar working pressure.
Flow Rate Optimization & Residue Reduction
Modern valve manufacturing balances rapid discharge velocity with precision flow control. Engineering optimized internal orifice geometries (DN50 2-inch and DN80 3-inch pathways) reduces batch discharge times by up to 28% while minimizing residual liquid left inside the bottle to less than 50 ml per 1000L tote.
Global Standardization & Compatibility
International chemical logistics demand strict adherence to ISO 22241, UN Markings, and standard thread pitches such as S60x6 Buttress and NPT fine threads. Selecting an experienced wholesale valve manufacturer guarantees seamless coupling compatibility across North American, European, and Asian transport networks.
Information Gain Insight for Sourcing Procurement Directors: Field testing data reveals that using sub-standard recycled polymer IBC valves increases micro-fissure stress cracking under hydraulic surge pressures by 43%. Sourcing direct from certified OEM factories utilizing 100% virgin High-Density Polyethylene (HDPE) and Glass-Filled Polypropylene (GFPP) reduces total cost of container ownership by eliminating in-transit product losses and costly container re-certification failures.
Material Science & Valve Anatomy Engineering
A detailed examination of material formulations, sealing elastomer physics, and valve mechanism designs utilized in modern IBC liquid discharge systems.
IBC Butterfly Valves
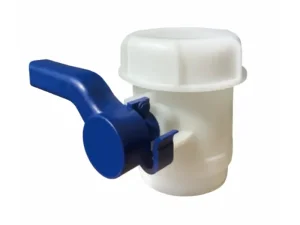
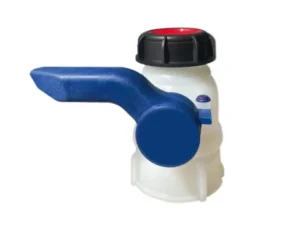
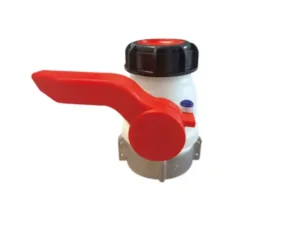
Constructed with a rotating HDPE disk mechanism held by a central spindle. Ideal for high-viscosity liquids, slurries, and general chemical storage where quick quarterly-turn operation and economical pricing are required.
- Size: DN50 (2") & DN80 (3")
- Thread: S60x6 / S100x8
- Low actuation torque required
IBC Ball Valves
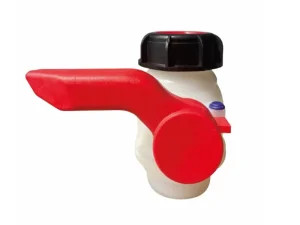
Featuring a spherical bore mechanism with PTFE seat rings. Provides exceptional seal integrity under aggressive chemical solvents, acids, and pressurized filling lines where zero friction wear is crucial.
- Full port smooth flow bore
- Reinforced PE stem shaft
- Anti-tamper aluminum foil seal ring
Stainless Steel Valves
Engineered with AISI 304/316L stainless steel for high-temperature, hygienic food-grade, or highly hazardous volatile chemical applications requiring fire-safe certified container valves.
- Welded or flange connection
- Autoclave-safe & SIP sterilizable
- Extreme corrosion resistance
Specialty Camlock Valves
Integrated male/female camlock quick-connect couplings designed for fast connection to flexible discharge hoses without requiring secondary threaded adapters.
- Type C & Type DC options
- Dust cap seal protection
- Vibration lock handles
| Material / Seal Type | Operating Temp (°C) | Chemical Resistance Profile | Typical Industrial Media Application |
|---|---|---|---|
| HDPE + EPDM Seal | -20°C to +70°C | Excellent for polar solvents, alkalis, dilute acids | Water treatment chemicals, agricultural liquid fertilizer |
| GFPP + FKM (Viton) Seal | -10°C to +90°C | Superior against hydrocarbons, aromatic solvents, concentrated acids | Petrochemical additives, automotive fluids, industrial solvents |
| HDPE + PTFE (Teflon) Seat | -30°C to +110°C | Universal chemical inertia across almost all aggressive chemicals | High-purity electronic chemical solutions, hazardous reagents |
| 316L Stainless Steel + PTFE | -40°C to +180°C | Full resistance to extreme temperature, organic acids, high pressure | Pharmaceutical intermediates, food-grade syrups, edible oils |
Tailored Fluid Control for Specialized Commercial Sectors
Different industries face unique regulatory compliance demands and material compatibility challenges. Our manufacturing facility engineers specialized valve configurations tailored to your sector.
1. Specialty Chemicals & Resins
Chemical processors require maximum corrosion defense against caustic soda, sulfuric acid derivatives, solvents, and polymers. We supply glass-reinforced polypropylene ball valves equipped with high-purity PTFE gaskets that eliminate environmental stress cracking and prevent seal degradation even under continuous exposure to aggressive reagents.
2. Food, Beverage & Ingredients
For edible oils, liquid fructose, dairy derivatives, and wine concentrates, hygiene is paramount. Our food-grade IBC valves are fabricated in cleanroom environments using 100% virgin FDA-compliant polymers (EU Regulation 10/2011 certified) with smooth internal fluid channels that prohibit bacterial growth and facilitate effortless clean-in-place (CIP) sanitation.
3. Agrochemicals & Fertilizers
Bulk fertilizers, liquid pesticides, and herbicides present high crystallization risks that can jam traditional discharge mechanisms. Our heavy-duty DN50 butterfly valves incorporate high-torque PE butterfly disks with self-cleaning seal geometries, guaranteeing smooth manual handle operation even after months of outdoor agricultural storage.
Rigorous Manufacturing & Testing Protocol
With over 26 years of specialized injection molding expertise, Linyi Dasheng operates three state-of-the-art production bases delivering unmatched quality control at every stage of production.
Precision Tooling & Mold Making
Our internal mold design center utilizes advanced CAD/CAM software and mold flow analysis to craft high-precision injection molds. CNC machining tolerances up to 0.005mm guarantee that every valve threads onto the IBC bottle neck with consistent sealing tension.
Hydrostatic Pressure Testing
Random batch samples undergo hydraulic pressure testing exceeding 2.5 bar for 30 minutes to verify frame structural resistance against water hammer spikes during long-distance bulk transport.
100% Pneumatic Leak Testing
Every single valve produced on our automated assembly lines undergoes an automated dry-air bubble leak check at 0.3 bar in both closed and half-open positions prior to secondary packaging.
Full Batch Traceability
Every shipment is tagged with a unique batch code detailing resin lot certificates, operator IDs, molding timestamps, and QC verification sign-offs for seamless ERP integration.
Customized Manufacturing & Rapid Global Dispatch
Supporting regional distributors, tote reconditioners, and multinational chemical enterprises with flexible OEM branding and localized technical compliance.
Custom OEM/ODM Branding
We provide full custom branding support including customer logo engraving on valve bodies, custom color-coded handles (Red, Blue, Black, Green), bespoke security seals, and customized outer cardboard packaging for private-label distributors.
International Thread Adapter Kits
To support global fleet logistics, we supply an extensive range of transition adapters converting standard S60x6 buttress threads to NPT, BSP, Camlock, or Hose Barb outlets, ensuring universal compatibility across North American, European, and Asia-Pacific discharge systems.
3-Day Dispatch Bulk Stock
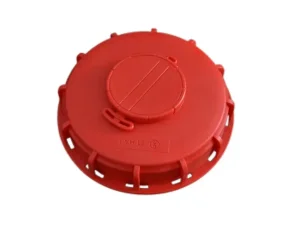
We maintain comprehensive warehouse inventories of standard DN50 ball valves, DN50/DN80 butterfly valves, breathable lids, and sealing covers, enabling fast 3-day dispatch for urgent replacement orders and container repair facilities.
The Future of Intelligent & Sustainable IBC Valve Technology
How our R&D team is driving innovation in circular packaging, zero-emission volatile organic compound (VOC) containment, and smart digital asset tracking.
IoT Smart Valve Integration
Integrating embedded RFID chips and NFC sensors directly into the valve body to track batch history, total discharge cycles, automated open/close status logs, and tamper verification across digital supply chains.
Zero-VOC Vapor Recovery Valves
Developing closed-loop dual-action vapor recovery valves that capture toxic organic vapors during high-speed chemical filling, protecting plant operators and ensuring strict environmental air safety compliance.
100% Recyclable Modular Assemblies
Eliminating non-recyclable composite inserts by engineering single-material polymer valves designed for quick automated disassembly, enabling 100% closed-loop recycling during tote reconditioning.
High-Torque Ergonomic Handles
Redesigning handle leverage profiles using carbon-fiber reinforced polyamides to lower manual opening force by 35%, improving operator safety in freezing outdoor depot conditions.
Frequently Asked Questions by Industrial Sourcing Teams
S60x6 is the coarse buttress thread standard across Europe and internationally for IBC tank outlets (60mm outer diameter with 6mm thread pitch). NPT (National Pipe Thread) is a tapered fine thread standard widely used in North America. We manufacture direct S60x6 valves as well as factory-fitted NPT conversion adapters to accommodate global container fleets.
Butterfly valves are lightweight, highly cost-effective, and ideal for standard water-based liquids, food syrups, and general non-aggressive chemicals. Ball valves feature a full-bore PTFE spherical seat that offers superior pressure resistance and absolute chemical inertia, making them the preferred specification for hazardous solvents, aggressive acids, and high-purity industrial chemicals.
Gaskets represent the primary sealing barrier. EPDM gaskets excel in polar solvents and dilute acids but degrade in contact with oils and hydrocarbons. Viton (FKM) gaskets provide excellent resistance to fuels, oils, and concentrated acids. PTFE (Teflon) offers universal chemical inertia across almost all aggressive industrial reagents. Matching gasket chemistry to your liquid medium prevents swelling, shrinkage, and premature valve failure.
Yes. Our heavy-duty IBC valves are engineered and certified to meet UN hazardous materials packaging requirements (UN 31HA1/Y designs). They undergo continuous drop tests, stacking tests, and hydrostatic pressure testing to ensure full compliance for ADR, RID, and IMDG transport regulations.
We offer comprehensive customization including handle color customization (red, blue, green, yellow, black), laser-engraved corporate branding, custom foil tamper seals, specialized thread sizes (DN50, DN80), custom polymer resin compounding (UV-inhibited or conductive anti-static PE), and specialized export packaging.
Our factory operates 3 specialized production bases with high-precision CNC tooling equipment (0.005mm machining tolerance). Every production line incorporates automated 100% dry-air bubble pneumatic testing at 0.3 bar, hydrostatic batch testing at 2.5 bar, and rigorous resin density verification under ISO 9001 quality management procedures.
Explore Secondary IBC Fittings & Accessories
High-performance replacement valves, breathable covers, and specialized tank accessories for global industrial buyers.