Featured Industrial IBC Tap Valves & Components
Explore our high-performance replacement valves, guide pipes, anti-sloshing baffles, and structural components built for rigorous chemical and industrial applications.
Global IBC Tap Valve Industry Trends & Macro Evolution
Analysis of changing chemical logistics compliance, sustainability imperatives, and next-generation fluid transfer technology.
The global intermediate bulk container (IBC) market is undergoing a seismic shift driven by strict international environmental regulations, dynamic supply chain demands, and unprecedented corporate emphasis on ESG (Environmental, Social, and Governance) transparency. At the epicenter of this evolution is the humble yet technically complex IBC tap valve assembly—the single critical point of control governing liquid integrity, operator safety, and zero-emission containment.
Material Science Innovation
Shift toward high-density polyethylene (HDPE) resins compounded with fluorinated barriers (Fluorination Level 5) to prevent solvent permeation and ESC (Environmental Stress Cracking) in aggressive chemical transport.
Hazardous Material Compliance
Strict enforcement of UN/DOT Packing Group I, II, and III certifications requires tap valves to withstand extreme pressure drops, hydrostatic stress, and drop impact tests down to -18°C.
Closed-Loop Circular Economy
Transition from single-use IBC totes to remanufactured, multi-trip reconditioned totes, demanding heavy-duty replacement valves engineered for easy thermal cleaning, disassembly, and seal replacement.
The Shift to High-Flow DN80 and Integrated Butterfly Architectures
Industrial procurement data reveals a accelerating transition from traditional DN50 (2-inch) standard discharge ports to specialized DN80 (3-inch) integrated butterfly and ball valves. High-viscosity fluids—including paints, adhesives, food slurries, and agricultural concentrates—demand expanded internal orifice geometries to eliminate flow bottlenecks, reduce tank unloading times by up to 45%, and minimize residual liquid waste.
Engineering Architecture & Chemical Compatibility Matrix
Precision component matching ensures long-term sealing integrity and prevents catastrophic fluid leaks.
Selecting the optimal wholesale IBC tap valve requires an in-depth understanding of elastomer degradation, thermal expansion rates, and chemical exposure parameters. Linyi Dasheng Import & Export Co., Ltd. manufactures injection-molded components utilizing virgin food-grade PE-HD, coupled with specialized seal materials optimized for specific chemical classes.
| Valve Component / Seal Type | Material Composition | Operating Temp Range | Chemical Resistance Profile | Recommended Applications |
|---|---|---|---|---|
| ETFE / PTFE (Teflon) Seals | Fluoropolymer Composite | -20°C to +120°C | Universal Chemical Inertness (Strong Acids, Solvents, Oxidizers) | Petrochemicals, High-Purity Acids, Solvents |
| EPDM Gaskets | Ethylene Propylene Diene | -40°C to +90°C | Excellent for Alcohols, Dilute Acids, Ketones, Steam | Water Treatment, Agricultural Chemicals, Food Slurries |
| FKM / Viton® Seals | Fluoroelastomer | -15°C to +180°C | High resistance to Hydrocarbons, Oils, Fuels, Chlorinated Solvents | Lube Oils, Fuel Additives, Industrial Solvents |
| DN50 / DN80 Valve Bodies | Virgin PE-HD / 316L Stainless | -30°C to +70°C | High impact resistance, UV resistance, zero stress-cracking | UN Bulk Liquid Transport Totes & Storage Drums |
Valve Mechanism Comparison: Butterfly vs. Ball Valves
Procurement teams must balance mechanical seal longevity against flow dynamics when specifying tote discharge configurations:
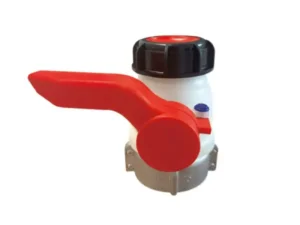
- Integrated HDPE Butterfly Valves: Cost-effective, compact design featuring a rotating disk mechanism. Ideal for general liquid logistics, water-based chemicals, and standard industrial fluids. Features low weight and robust thermal stability.
- Welded & Threaded Ball Valves: Feature a spherical closure element providing a straight-through flow path with zero flow resistance. Best suited for high-viscosity liquids, aggressive organic solvents, and applications requiring fine metering or rapid emergency shutoff.
Global Corporate Procurement Needs & Sourcing Framework
Mitigating supply chain risks, verifying vendor credentials, and securing total cost of ownership (TCO) optimization.
For international supply managers, chemical manufacturers, and IBC reconditioners, sourcing replacement parts and OEM valves from overseas suppliers involves rigorous quality control audits and risk management protocols. A single valve failure during cross-border maritime container transport can lead to tens of thousands of dollars in lost cargo, hazmat cleanup costs, and regulatory fines.
0.005mm Tooling Precision
In-house mold design and mold flow analysis eliminate flash, warpage, and thread pitch misalignment, ensuring seamless compatibility with Schuetz, Mauser, Greif, and standard UN 1000L totes.
Fast Rapid-Dispatch Stocking
With 3 integrated manufacturing bases in Shandong, standard DN50/DN80 replacement parts and guide pipes maintain high buffer stock for dispatch within ~3 days of purchase orders.
Custom OEM/ODM Branding
Tailor-made colors, customized company logos molded directly into handles or valve bodies, specialized thread adapters (Camlock, BSP, NPT), and complete private label solutions.
Cost-per-Cycle Evaluation Model for B2B Purchasing
When evaluating wholesale pricing, leading enterprise buyers use a total cost of ownership (TCO) calculation rather than initial unit purchasing cost:
By using 100% virgin resin, stainless steel spring reinforcement inserts, and precision pressure testing, Linyi Dasheng valves deliver up to 3x higher cycle life, dramatically slashing the overall TCO for container fleet managers.
Macro Industry Solutions & Turnkey Application Scenarios
Tailored bulk liquid management configurations engineered for specialized market sectors.
Petrochemical & Fine Chemicals
Challenge: Volatile organic compounds (VOCs) and aggressive solvents degrading standard rubber gaskets, causing slow leaks during long ocean transit.
Solution: DN50/DN80 integrated PTFE-sealed valves paired with anti-sloshing internal baffles and stainless steel spring inserts to maintain dynamic pressure resistance under continuous vessel vibration.
Food & Beverage Processing
Challenge: Risk of bacterial harborage, contamination, and non-compliance with international food-contact hygiene standards.
Solution: FDA and EU 10/2011 compliant virgin PE-HD valves produced in cleanroom conditions, featuring smooth internal bores without dead zones, facilitating clean-in-place (CIP) steam sterilization.
Agricultural Chemicals & Fertilizers
Challenge: Highly corrosive pesticide concentrates and liquid nitrogen fertilizers causing rapid stress-cracking in non-UV-stabilized plastics.
Solution: Heavy-duty UV-inhibited polymer valve assemblies fitted with breathable pressure-relief caps to vent off-gassing chemicals safely while preventing external rain or particulate ingress.
Regulatory Compliance & Global Quality Assurance
Rigorous testing standards ensuring international market acceptance and hazardous material transportation safety.
Navigating cross-border logistics requires strict adherence to international standardizations. Our manufacturing facilities in Linyi, Shandong operate under an integrated ISO 9001:2015 quality management system, enforcing multi-stage quality control checks throughout the raw material compounding, injection molding, and assembly steps.
Key Testing Protocols Conducted on Every Batch:
- Hydrostatic Leakage Testing: Valve assemblies are submerged and pressurized up to 30 kPa (0.3 bar) for extended periods to verify bubble-tight sealing.
- Drop & Impact Resistance: Finished valves mounted to 1000L test totes are conditioned at -18°C and subjected to 1.9-meter drop tests in accordance with UN Hazardous Materials Transport regulations.
- Thread Torque & Mechanical Fatigue Testing: Handles and valve stems undergo 5,000+ continuous open-close mechanical cycles under pressurized load to ensure smooth operation without stem shear or seat deformation.
- Chemical Compatibility & Immersion Validation: Test samples are immersed in concentrated nitric acid, sodium hydroxide, and toluene for 28 days to measure mass swell and tensile strength retention.
Technical Roadmap & Future Outlook (2025–2030)
Emerging technologies shaping the next decade of intelligent, zero-emission bulk fluid management.
As industrial automation, IoT monitoring, and carbon neutralization goals reshape global manufacturing, the humble IBC tap valve is evolving into a smart, data-enabled asset. Linyi Dasheng is actively investing in research and development to bring next-generation smart packaging solutions to global suppliers.
IoT-Enabled Smart Valves
Integration of wireless micro-sensors into valve handles to provide real-time telemetry on valve position (open/closed), fluid flow rate, internal pressure, and unauthorized tamper detection via RFID/NFC protocols.
Bio-Based & Recycled Polymers
Development of chemically modified post-consumer recycled (PCR) resin compounds and bio-HDPE matrices that maintain 100% of structural integrity while cutting cradle-to-gate carbon footprints by up to 40%.
Zero-Fugitive Emission Sealing
Patented double-eccentric stem seals and magnetic levitation valve actuators engineered to comply with upcoming European chemical logistics zero-leakage standards.
Enterprise Q&A: Frequently Asked Questions
Technical guidance and commercial clarity for procurement directors, logistics engineers, and distributor buyers.
What products does Dasheng manufacture for wholesale IBC tank users?
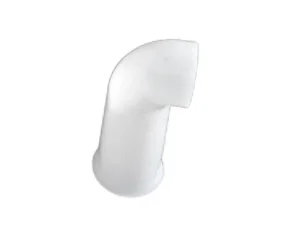
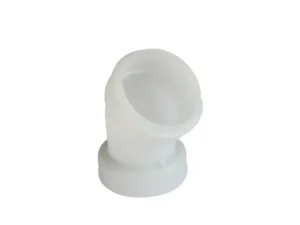
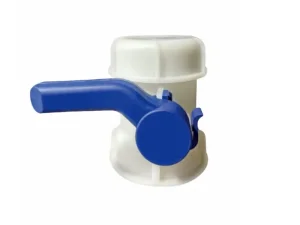
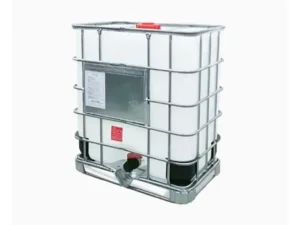
Linyi Dasheng Import & Export Co., Ltd. manufactures and exports complete 1000L heavy-duty IBC containers, integrated DN50/DN80 butterfly and ball valves, replacement valve guide pipes, red breathable vent caps, black gasketed sealing lids, galvanized crossbeam support bars, plastic anti-sloshing baffles, aluminum pallet bases, stainless steel nameplates, and custom injection-molded fittings.
How do I determine whether my application requires a DN50 or a DN80 IBC valve?
Choose a DN50 (2-inch) valve for standard liquid transfer (water, oils, general chemicals) where standard flow rates are acceptable. Upgrade to a DN80 (3-inch) high-flow valve when handling viscous liquids (resins, slurries, molasses, heavy coatings) or when rapid container emptying is required to optimize plant turnover speed.
Can Dasheng customize threads, colors, and logos for OEM replacement valve orders?
Yes. We offer comprehensive OEM/ODM services including custom mold tooling, color matching (standard blue, black, red, yellow, green), custom branding molded into handles/bodies, and specialized thread configurations (S60x6 buttress, S100x8 coarse thread, BSP, Camlock quick-connect couplings, NPT male/female outlets).
How fast is your manufacturing lead time and global dispatch for bulk valve orders?
For standard IBC valves, replacement caps, and guide pipes, we maintain extensive ready-to-ship buffer stock in our Shandong warehouses, permitting fast order fulfillment in approximately 3 business days. Custom OEM tooling, non-standard colors, or volume container shipments are completed within 15–20 days under strict contractual delivery terms.
What sealing materials are available to handle aggressive acids and aromatic solvents?
We configure valve seats with specialized elastomers based on chemical compatibility requirements. For high-purity acids, aggressive solvents, and volatile hydrocarbons, we provide PTFE (Teflon) or FKM (Viton®) seals. For food products, mild alkalis, and aqueous solutions, we provide food-grade EPDM or NBR seals.
Complete Container Storage, Pallets & Accessories Range
Explore our complete inventory of industrial ball valves, vertical tanks, plastic pallets, and high-strength lid fasteners.
Partner with China's Premier IBC Tap Valve Manufacturer
Contact our engineering sales team today to request CAD models, material chemical resistance charts, volume wholesale price breaks, or sample evaluation kits.