Featured Industrial IBC Fittings & Valves
Direct factory-grade components engineered for high-density polyethylene (HDPE) bulk containers, ensuring zero-leak liquid handling across global hazardous and non-hazardous supply chains.
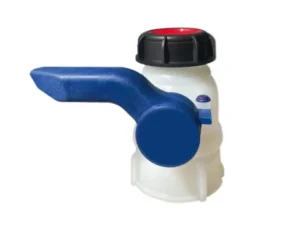
The Evolution & Macro Market Dynamics of Industrial IBC Valves
Intermediate Bulk Containers (IBCs) serve as the backbone of global industrial liquid logistics, moving billions of liters of high-purity chemicals, food-grade ingredients, lubricants, and agricultural concentrates annually. At the heart of every 1000-liter tote lies a critical component: the IBC Ball Valve. Operating under harsh mechanical stress, chemical exposure, and dynamic temperature ranges, these valves are no longer considered simple closure devices; they are precision-engineered safety units designed to eliminate catastrophic leaks and reduce volatile organic compound (VOC) emissions.
Information Gain Insight: According to global bulk packaging market analyses, failure rates in liquid logistics stem primarily from valve seal degradation (42%) and thread stress cracking (28%). Modern wholesale sourcing mandates high-performance polymers like glass-reinforced polypropylene (PP-GF30) and chemical-grade PTFE/FKM seals to withstand dynamic transport vibrations.
Shift to Integrated Molded Valves
Traditional threaded valve attachments are increasingly replaced by blow-molded or ultrasonic-welded integrated flange systems. This structural integration eliminates threaded seal leak paths, drastically improving integrity during long-distance multimodal freight transport.
UN Hazardous Compliance
International dangerous goods regulations (ADR, RID, IMDG) enforce stringent drop-impact and hydraulic pressure ratings. Modern IBC factories implement 100% pneumatic testing for every DN50 ball valve leaving the assembly line.
Circular Economy & Reuse
With environmental packaging levies expanding across Europe and North America, IBC totes are reconditioned up to 5–10 cycles. High-durability ball valves feature replaceable internal seals and heavy-duty safety latches to maximize tote service lifespan.
Technical Architecture: Materials, Tolerances & Flow Dynamics
Selecting a wholesale IBC ball valve requires evaluating mechanical shear, thermal expansion coefficient, and chemical compatibility matrix. Below is an engineering benchmark outlining material selection for high-performance valve assembly.
| Component | Standard Polymer Material | High-Chemical Grade Option | Key Performance Attribute |
|---|---|---|---|
| Valve Body | Polypropylene + 30% Glass Fiber (PP-GF30) | High-Density Polyethylene (HDPE) / PVDF | High tensile strength, zero stress cracking, heat stability to 90°C |
| Internal Ball Core | Polypropylene (PP) / Polyoxymethylene (POM) | 316 Stainless Steel / High-Purity PTFE | Smooth operation torque, cavitation resistance, chemical inertness |
| Primary Gasket & Seals | EPDM (Ethylene Propylene Diene Monomer) | FKM (Viton) / Encapsulated PTFE | Resistance to aggressive solvents, acids, oils, and aromatic hydrocarbons |
| Handle & Safety Lock | Reinforced ABS / High-Impact PP | Stainless Steel Handle with Safety Latch | Prevents accidental discharge during high-vibration truck transport |
| Thread Standards | S60x6 Male Buttress Thread | NPT / BSP / Camlock Adapter Interfaces | Universal connection compatibility for European & American discharge hoses |
Flow Rate & Cavitation Control (Cv Coefficient)
Engineered DN50 (2-inch) and DN80 (3-inch) ball valves feature an optimized internal bore profile that minimizes fluid turbulence. Full-port design maintains a high flow coefficient ($C_v$), allowing viscosity-heavy fluids like resins, liquid fertilizers, and syrups to discharge rapidly without vacuum buildup or pump cavitation.
Double-Lock Anti-Leak Mechanism
Our OEM factory incorporates a dual-stem seal ring assembly paired with an extra-wide dust cap seal. Even under extreme hydraulic surge pressures (water hammer effect up to 0.4 MPa), the secondary sealing chamber prevents micro-seepage, safeguarding hazardous cargo.
Global Buyer Demand & Total Cost of Ownership (TCO)
For enterprise procurement officers and industrial packaging distributors, selecting a wholesale IBC valve supplier goes beyond initial unit price. Operating costs, warranty claim rates, container re-usability, and tariff resilience dictate long-term profitability.
Supply Chain Consolidations
Global buyers are transitioning from multi-vendor component sourcing to integrated single-source manufacturers capable of delivering complete IBC assemblies: inner bottles, cages, lids, pallets, nameplates, and valves under a unified quality audit.
Custom OEM Color & Branding
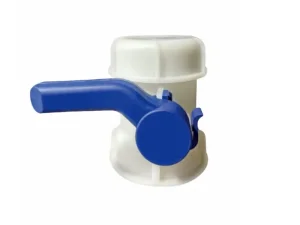
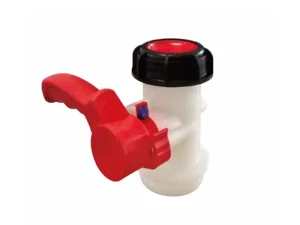
Corporate chemical brands increasingly demand custom color-coded valve handles (e.g., Red for hazard venting, Blue for food-grade, Black for general chemicals) alongside laser-engraved serial batch codes for digital fleet tracking.
Zero-Defect Quality Assurance
Automated high-speed injection molding combined with robotic leak-detection guarantees a defect rate below 50 PPM (Parts Per Million), mitigating costly environmental cleanup claims overseas.
Tailored Fluid Control Solutions Across Global Sectors
Industrial applications present distinct chemical, thermal, and regulatory challenges. Our factory produces custom-configured valve assemblies engineered for specific chemical matrix categories.
Chemical & Hazardous Materials
Equipped with pure PTFE ball seats and FKM Viton gaskets, our chemical-grade valves resist swelling, cracking, or leaching when exposed to solvents, mild acids, caustic alkalis, and industrial cleaning agents. Features anti-static grounding pin options for explosive zone transport.
Food & Beverage Sanitary Transfer
Manufactured using virgin FDA-compliant food-grade Polypropylene resin. Free from heavy metals, phthalates, and BPA. Paired with food-grade EPDM seals, these valves handle liquid sugar, vegetable oils, wine, dairy derivatives, and fruit juice concentrates without contamination.
Agricultural Liquid Fertilizer & Pesticides
Agricultural chemicals generate severe outdoor UV degradation and crystallization inside valve seats. Our UV-stabilized carbon-black formulation combined with quick-cleaning ball cavities prevents salt buildup and ensures smooth valve lever movement after seasonal storage.
Lubricants, Adhesives & Heavy Oils
Viscous motor oils, silicone fluids, and industrial glues require robust torque handles and wide discharge nozzles. DN80 integrated butterfly and ball valves provide unhindered discharge paths that prevent clogging during cold-weather emptying.
Quality Control Infrastructure & Factory Compliance
Operating three state-of-the-art production bases covering tens of thousands of square meters in Linyi, Shandong, Linyi Dasheng Import & Export Co., Ltd. integrates specialized mold fabrication with automated injection molding and assembly lines.
0.005mm Precision Tooling
In-house CNC mold design and mold flow simulation guarantee ultra-tight tolerances. Precise mold alignment eliminates flash and surface irregularities on sealing surfaces that lead to seal fatigue.
Pneumatic & Hydraulic Testing
Every individual valve unit undergoes positive-pressure air submerged leak detection at 0.2 MPa (2 Bar) for a minimum of 15 seconds, followed by sample destruction burst pressure testing up to 0.8 MPa.
Global Export Certification
Our production system operates under ISO 9001 quality management guidelines. Products comply with REACH, RoHS, FDA food-contact standards, and UN dangerous packaging specifications.
Technology Roadmap: Smart Valves & Next-Gen Polymers (2026–2030)
As global supply chains undergo digital transformation and decarbonization, the industrial packaging sector is evolving rapidly. Our R&D team is pioneering next-generation valve technologies that merge smart telemetry with sustainable materials.
IoT-Enabled Smart Valves
Integration of passive RFID and low-power Bluetooth sensors directly into the valve handle housing. Provides real-time tamper evidence, valve open/close count logging, and automated batch identification during filling and emptying cycles.
Bio-Based Polypropylene Resins
Pioneering chemical recycling and bio-attributed polymers derived from tall oil and agricultural waste feedstocks. Reduces the embedded carbon footprint of each valve by up to 45% without sacrificing tensile strength or chemical resistance.
Modular Fast-Exchange Core
Developing patented modular internal valve cores that allow tote reconditioners to swap internal ball seals in under 30 seconds without damaging the blow-molded bottle neck connection.
Frequently Asked Technical & Sourcing Questions
Deep dive technical answers for packaging engineers, quality auditors, and procurement managers.
What is the difference between an IBC ball valve and an IBC butterfly valve?
How do I determine whether I need DN50 or DN80 sizing for my IBC tanks?
Which gasket seal material (EPDM, FKM, or PTFE) should be specified for aggressive solvents?
What are the standard thread connection types available for export order customization?
Can Linyi Dasheng support OEM custom logo engraving and color-coded handles?
What lead times and minimum order quantities (MOQ) apply for direct factory wholesale?
IBC Tank Lids, Guide Pipes & Specialized Adapters
Explore additional factory-direct replacement fittings, protective lids, spill containment solutions, and custom accessories for complete IBC fleet maintenance.
Partner with China's Leading IBC Fitting Manufacturer
Linyi Dasheng Import & Export Co., Ltd. supplies global packaging distributors, reconditioners, and chemical enterprises with precision-molded IBC ball valves, lids, bases, and complete containers. Contact our engineering support team for instant technical drawings, bulk price quotes, and CAD samples.