Heavy Duty IBC Totes & Specialized Fittings
Direct factory wholesale catalog engineered for extreme mechanical strength, chemical inertness, and UN-rated dangerous goods transport compliance.
Global Industrial Fluid Logistics & High-Integrity Containment
Analyzing total cost of ownership (TCO), environmental compliance, and structural performance standards in global bulk packaging.
UN & Hazardous Goods Certification
Modern chemical logistics demands UN 31HA1/Y packaging ratings capable of withstanding hydraulic internal pressure tests exceeding 100 kPa and drop tests at extreme temperatures (-18°C). Heavy-duty composite IBCs eliminate environmental stress cracking (ESC) vulnerabilities during intermodal transit.
Volumetric Efficiency & Freight TCO
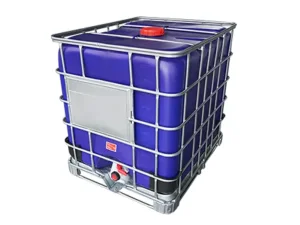
Compared to traditional 200L steel drums, a 1000-liter Heavy-Duty IBC container optimizes container payload by 35% per ISO sea freight container. The cube architecture minimizes unused void space, reducing freight-per-liter costs while simplifying automated forklift stack management up to 4-high.
Zero-Contamination Closed Loops
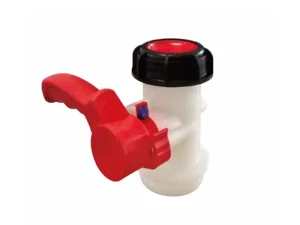
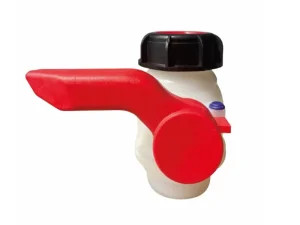
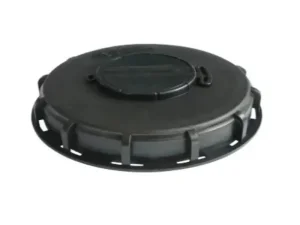
Equipped with specialized integrated butterfly and ball valves (DN50/DN80), fluorinated anti-permeation inner bottles, and secondary containment lids, heavy-duty IBC units protect high-purity agricultural chemical formulations and food-grade concentrates from atmospheric oxidation.
Advanced Polymer Processing & Engineering Matrix
Delivering maximum structural rigidity, chemical resistance, and thermal endurance through high-density polymer engineering.
As a leading wholesale heavy duty IBC tank manufacturer and direct supply factory, our engineering framework relies on High Molecular Weight High-Density Polyethylene (HMW-HDPE). This specialized thermoplastic polymer provides an extraordinary balance of Environmental Stress Crack Resistance (ESCR), tensile strength, and impact energy absorption across dynamic operating temperatures (-40°C to +60°C).
1. Multi-Layer Co-Extrusion & Gas Barrier Technology
Standard single-layer containers often fail when storing aggressive aromatic hydrocarbons, organic solvents, or halogenated compounds. Our multi-layer blow-molding technology integrates up to six distinct layers into a single homogeneous container wall:
- Outer Structural Layer: UV-stabilized virgin HDPE compounded with carbon black or specialized blue color masterbatch to prevent photo-degradation and thermal breakdown from solar radiation.
- Regrind/Reinforcing Core: High-density polyolefin blend engineered for maximum compressive load capacity, supporting multi-tier stacking during long-term storage.
- Permeation Barrier Layer: Ethylene Vinyl Alcohol (EVOH) or Fluorinated inner boundary that dramatically reduces hydrocarbon vapor transmission rates (VTR) to virtually zero.
- Inner Pure Layer: 100% FDA-compliant pure virgin HDPE guaranteeing zero contaminant leaching, certified for high-purity pharmaceutical intermediates and food concentrates.
2. Cage Architecture & Structural Frame Mechanics
The external protective cage serves as the primary load-bearing scaffold during transport and stacking operations. We utilize automated robotic welding lines to fabricate outer grid structures from zinc-coated tubular galvanized steel. Finite Element Analysis (FEA) computer simulations dictate the optimum cross-pipe pitch, transom alignment, and corner gusset placement.
| Engineering Metric | Standard Grade IBC Totes | Heavy Duty Factory IBC Totes | Testing Protocol / Compliance |
|---|---|---|---|
| Inner Bottle Resin Grade | Standard HDPE (MFI: 0.35 g/10min) | HMW-HDPE (MFI: 0.05 - 0.12 g/10min) | ASTM D1238 / ISO 1133 |
| Maximum Stacking Load | Under 2,200 kg (2-High Limit) | Up to 4,600 kg (4-High Dynamic Stacking) | ISO 16495 / UN Transport Regs |
| Hydraulic Internal Test Pressure | 100 kPa for 10 minutes | 200 kPa for 30 minutes (Zero Deflection) | UN 31HA1/Y Requirements |
| Venting & Pressure Relief | Manual Dust Cap | Automatic Breather Membrane (EPDM/PTFE) | FDA / EC 1935/2004 Sealed Safety |
| Base Pallet Material Options | Softwood / Reprocessed Plastic | Galvanized Steel / Aluminum / Heavy Duty HDPE | ISPM-15 Phytosanitary Exempt |
3. Precision Valve & Closure Integrity
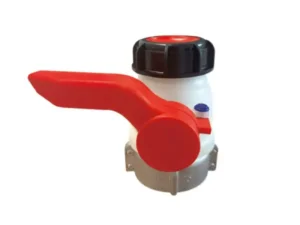
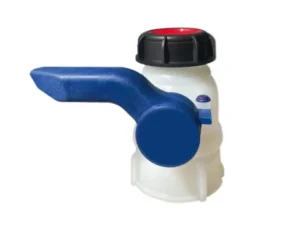
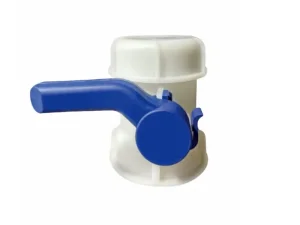
The bottom discharge outlet represents the most critically stressed component of any bulk liquid container. Our integrated DN50 (2-inch) and DN80 (3-inch) welded butterfly and ball valves are manufactured via high-precision injection molding machines operating at dimensional tolerances within 0.005 mm. Standard sealing materials include EPDM, NBR, Viton (FKM), and expanded PTFE encapsulations, offering universal chemical compatibility against acids, alkalis, esters, and mineral oils.
China Factory Infrastructure & Manufacturing Efficiency
Leveraging deep industrial cluster advantages, vertical integration, and advanced automation to deliver unbeatable wholesale values.
Vertical Integration & Tooling Control
From custom mold design and mold flow analysis to precision metal stamping and injection molding, Linyi Dasheng maintains complete control over the production ecosystem. In-house mold fabrication reduces OEM development timelines by up to 50% compared to outsourced suppliers.
Linyi Logistics & Port Accessibility
Located in Shandong’s primary logistics hub, our manufacturing facilities feature immediate access to major national highway networks and direct freight corridors to Qingdao Port. This proximity enables rapid bulk raw material procurement and seamless container dispatch within 3 days for standard stock orders.
Scale Economies & Raw Material Sourcing
Bulk purchasing contracts with global petrochemical leaders ensure top-tier virgin polymer supplies at highly competitive rates. Coupled with 24/7 automated blow-molding lines, our factory achieves exceptional economies of scale that are directly passed to international wholesale buyers.
Localized Application Scenarios Across Key Sectors
Engineered to adapt to demanding localized climate conditions, strict regional environmental laws, and diverse operational requirements.
Petrochemicals & Hazardous Solvents
In North American and European industrial hubs, our UN-certified Heavy Duty IBC tanks are deployed for transporting hazardous liquids, solvents, lubricants, and fuel additives. Anti-static conductive outer layers eliminate electrostatic discharge risks during flammable fluid pumping.
Agrochemical Formulations & Liquid Fertilizers
For agricultural regions in South America and Southeast Asia, our UV-resistant blue and black light-proof IBC totes protect sensitive liquid fertilizers, pesticides, and growth regulators from photo-chemical degradation and ambient heat buildup during farm storage.
Food-Grade Liquid Ingredients & Syrups
Utilized extensively in food processing facilities worldwide. Certified clean-room manufactured HDPE bottles paired with hygienic welded butterfly valves ensure sanitary transfer of fruit juices, edible oils, fructose syrups, and liquid food additives in full compliance with FDA regulations.
Regulatory Assurance & Full OEM/ODM Customization
Ensuring complete peace of mind through international certifications and tailor-made engineering services.
Regulatory Assurance & Certification
Every Heavy-Duty IBC container produced in our manufacturing base undergoes batch-wise quality inspections before leaving the loading bay. We maintain comprehensive compliance documentation to support your customs clearance and local environmental audits:
- UN Dangerous Goods Certification: Marked under UN 31HA1/Y for liquid density ratings up to 1.9 g/cm³.
- FDA & EC 1935/2004 Compliance: Migration test certificates confirming zero harmful plasticizer transfer in food applications.
- REACH & RoHS Compliance: Heavy metal free, phthalate free, and manufactured with 100% recyclable polyolefin materials.
Tailor-Made OEM/ODM Customization
We work closely with chemical brand owners, packaging distributors, and logistics fleet operators to build custom-branded fluid containers:
- Custom Molded Logos & Colors: Embossed corporate branding, custom color-coded lids (Red, Black, Blue, Yellow), and unique bottle hues.
- Engraved Stainless Steel Nameplates: Permanent laser-etched metal plates displaying barcode data, tare weight, batch numbers, and tracking information.
- Specialized Outlets & Adapters: Custom DN50/DN80 valve configurations, Camlock quick couplings, threads (S60x6, BSP, NPT), and dip tube filling systems.
Frequently Asked Technical & Purchasing Questions
Clear, definitive answers from our technical engineering team regarding IBC tote selection, maintenance, and ordering.
What sets Heavy-Duty IBC Totes apart from standard lightweight totes?
How do I choose between a Breathable Vented Cap and an Airtight Sealing Cap?
Are your IBC valves compatible with standard European and American discharge hoses?
What is the typical production lead time and minimum order quantity (MOQ)?
How does fluorination treatment enhance chemical barrier performance?
Valves, Frames & Component Replacement Lineup
High-precision replacement components manufactured to keep your container fleet operating at peak efficiency.
Partner with China’s Leading Heavy Duty IBC Manufacturer
Streamline your bulk liquid container supply chain today. Connect with our senior packaging engineers for custom mold designs, UN certification datasheets, and direct factory container pricing.
Request Factory Direct Wholesale Pricing