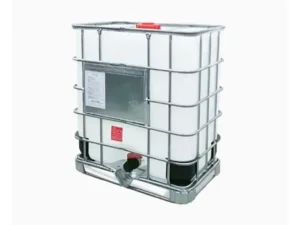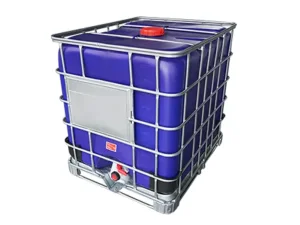
Featured Industrial IBC Components & Full Kits
Precision-engineered intermediate bulk container solutions manufactured under ISO 9001 quality frameworks.
Global Industrial Container Economics & China Sourcing Dynamics
Analyzing the shift toward modular, standardized 1000L IBC tank full kits in modern chemical supply chains and logistics infrastructure.
The Paradigm Shift in Liquid Bulk Logistics
The global industrial liquid packaging market has underwent a decisive transformation from rigid steel drums and ISO tank containers toward high-efficiency 1000-Liter Composite Intermediate Bulk Containers (IBCs). Driven by strict ESG (Environmental, Social, and Governance) requirements and optimized cubic utilization in standard 40ft ISO sea containers, the "Full Kit" approach—combining HDPE bottle, structural cage, valve assembly, and degassing lid—delivers up to 35% reduction in freight logistics costs per unit volume compared to traditional 200L drum configurations.
China Supply Chain Optimization & Quality Parity
Chinese original equipment manufacturers (OEMs) have elevated manufacturing capability beyond low-cost production into advanced engineering leadership. Leveraging integrated petro-chemical value chains, automated high-capacity blow molding machines, and precision zinc galvanizing lines, top-tier Chinese factories yield IBC full kits that comply seamlessly with UN Dangerous Goods Regulations (UN 31HA1) while reducing Total Cost of Ownership (TCO) by 22–30% for international distributors and chemical conglomerates.
Anatomy of an Industrial IBC Tank Full Kit
Comprehensive multi-layer engineering analysis of components designed for zero-leakage fluid transfer and extreme physical endurance.
1. Inner HDPE Container Bottle
Extrusion-blow-molded using virgin High-Density Polyethylene (HDPE) with ultra-high molecular weight resin distribution. Incorporates anti-UV additives, carbon black formulations, or multi-layer EVOH gas permeation barrier options. Optimized wall thickness control guarantees superior Environmental Stress-Crack Resistance (ESCR) against aggressive solvents, acids, and alkalis.
2. Tubular Steel Frame & Base Pallet
Constructed from hot-dip galvanized robotically-welded steel tubing arranged in a grid matrix optimized by Finite Element Analysis (FEA). Designed to resist lateral swell during high-density fluid containment. Dynamic stacking strength allows up to 4-high static loads, paired with composite, galvanized steel, or lightweight aluminum forklift-accessible pallets.
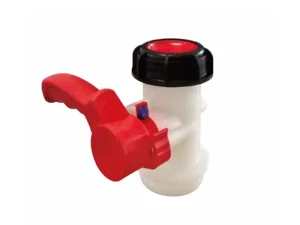
3. Integrated Discharge Valve Assembly
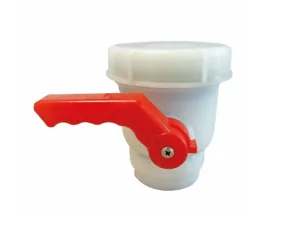
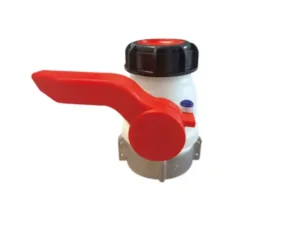
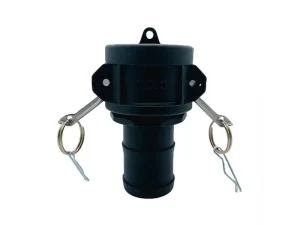
Available in DN50 (2-inch) and DN80 (3-inch) nominal diameters. Options include sanitary welded butterfly valves and full-bore ball valves manufactured from high-purity polypropylene, polyethylene, or AISI 316 Stainless Steel. Features advanced seal chemistries including EPDM, ETFE, PTFE, and Viton (FKM) for leak-proof seal integrity.
Standardized Product Variants Comparison
Engineering parameters to assist procurement teams in matching chemical characteristics with proper kit configurations.
| Kit Configuration Type | Inner Liner Material | Gasket / Seal System | UN Dangerous Rating | Primary Industrial Use Case |
|---|---|---|---|---|
| Standard 1000L Translucent Kit | Virgin HDPE (Natural translucent) | EPDM / Polypropylene | UN 31HA1/Y (SG ≤ 1.6) | General Industrial Chemicals, Water Treatment, Agrochemicals |
| UV-Resistant Light-Proof Kit | HDPE + Carbon Black / Blue Opaque | Viton (FKM) / PTFE | UN 31HA1/Y (SG ≤ 1.9) | Light-Sensitive Chemicals, Resins, Photosensitive Actives |
| High-Permeation Barrier Kit | Co-extruded HDPE + EVOH Layer | PTFE Encapsulated | UN 31HA1/Z (SG ≤ 1.9) | Aromatic Hydrocarbons, Solvents, Flavorings, Essences |
| Sanitary Food-Grade Kit | FDA-Compliant Virgin HDPE | Food-Grade Silicone / EPDM | Non-Hazardous / FDA Certified | Liquid Food Ingredients, Concentrates, Edible Oils, Syrup |
| Stainless Steel Valve Hybrid Kit | Heavy-Duty Reinforced HDPE | AISI 316 Stainless / PTFE | UN 31HA1/Y (SG ≤ 2.1) | Highly Aggressive Acids, Organic Solvents, High-Temp Liquids |
Localized Deployment & Sector Applications
How leading global chemical plants, agricultural hubs, and processing units implement Chinese IBC kits.
Petrochemicals & Fine Chemicals
In North American and European industrial parks, strict storage safety mandates require continuous static dissipation and chemical inertia. Chinese-manufactured EX-rated anti-static IBC kits featuring grounded grounding cables and inner conductive layers prevent electrostatic discharge when handling volatile organic compounds (VOCs).
Agrochemicals & Crop Protection
In tropical agricultural markets across Southeast Asia and South America, high UV radiation breaks down low-grade containers. Heavy-duty black opaque and blue UV-blocking IBC kits preserve active pesticide, herbicide, and liquid fertilizer formulations against photochemical degradation while enduring high ambient humidity.
Lithium-Ion Battery Electrolyte Transport
The global EV battery manufacturing ecosystem demands ultra-pure, zero-moisture transport systems. Specialized fluorinated and high-purity stainless-valve IBC kits ensure zero trace-metal contamination during movement of lithium hexafluorophosphate (LiPF6) liquid electrolytes between chemical refineries and gigafactories.
UN 31HA1 Regulatory Compliance & Stress Testing
rigorous validation procedure executed on every factory production batch to ensure zero failure rates during transit.
1. Pneumatic & Hydraulic Pressure Tests
Every inner container undergoes automated pneumatic leak testing at 20 kPa (3.0 PSI) pressure for a minimum of 10 seconds. For UN dangerous goods certification, random batch samples undergo hydraulic internal pressure testing reaching 100 kPa to 200 kPa for 10 minutes without wall rupture or joint leakage.
2. Cold-Temperature Drop Test Matrix
Conditioned at -18°C (0°F) to evaluate low-temperature brittle fracture performance. Containers fully loaded to capacity are dropped from heights ranging from 1.2 to 1.9 meters onto a solid, non-resilient steel impact surface at multiple angle orientations (diagonal bottom corner impact, side impact, and valve base direct impact).
3. Dynamic Vibration & Stacking Test
Simulating long-haul sea freight and intermodal transport vibration. The full kit is subjected to dynamic multi-axis mechanical vibration at 4.7 Hz for 60 minutes, followed by top-load compression testing exceeding 28 days under elevated temperatures (40°C) simulating maximum stack weights up to 4,600 kg.
4. Environmental Stress-Crack Resistance (ESCR)
Samples taken from the bottle wall are immersed in active surface-agent solutions (such as 10% Igepal CO-630) under 50°C ambient environments under constant mechanical stress. Standard compliance dictates continuous exposure exceeding 1,000 hours without micro-fissure development.
Technology Roadmap: Next-Gen Smart & Sustainable IBC Kits
Strategic innovations driving the next decade of industrial container manufacturing in China.
PCR Polymer Blends
Integration of up to 30% Post-Consumer Recycled (PCR) HDPE in non-contact middle bottle layers without compromising mechanical UN load capability.
IoT Telematics Integration
Embedded cellular/LoRaWAN sensor caps monitoring liquid volume, real-time temperature, internal pressure, tilt angles, and GPS location tracking.
Ultra-Light Metal Alloys
Transition from standard galvanized steel cages to high-tensile lightweight alloy frames, reducing unit tare weight by up to 14 kg per full kit.
Closed-Loop Reconditioning
Standardized modular quick-release valve fittings to accelerate bottle wash, decontamination, and bottle replacement in global reconditioning loops.
Frequently Asked Questions for Procurement Engineers
Detailed technical insights resolving common engineering and sourcing questions regarding Chinese IBC tank full kits.
Explore Full IBC Containers & Specialized Accessories
Direct factory supply for high-capacity liquid storage containers, light-proof bottles, and replacement components.