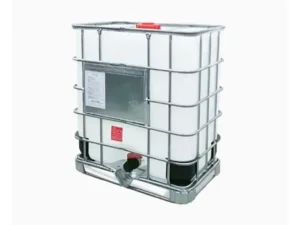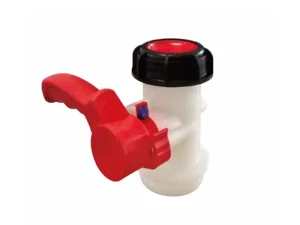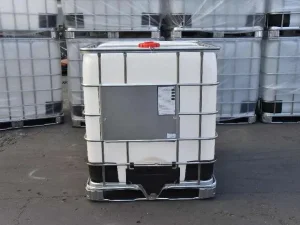
Featured Industrial DN80 & Bulk Container Solutions
Direct factory supply featuring heavy-duty butterfly valves, welded ball valves, replacement caps, and structural accessories engineered to international UN and ISO standards.
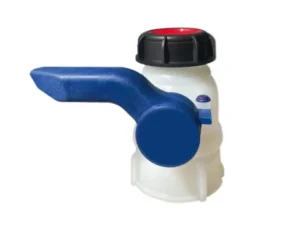
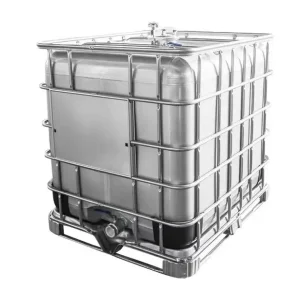
The Strategic Imperative of DN80 (3-Inch) Valves in Modern Bulk Logistics
In global liquid supply chains, discharge speed, structural integrity, and chemical zero-leakage are critical operational metrics. As a premier China DN80 IBC valve supplier, we explore the transition from standard DN50 (2-inch) to heavy-duty DN80 (3-inch / 80mm) discharge systems.
The DN80 valve internal bore diameter (80mm) provides a cross-sectional flow area of approximately 5,026 mm², compared to just 1,963 mm² in a standard DN50 valve. This hydrodynamic increase cuts liquid discharge time by up to 60%, allowing rapid unloading of high-viscosity liquids, slurries, latex, resins, and food-grade syrups in automated industrial plants.
Industrial intermediate bulk containers (IBCs) experience severe hydrodynamic sloshing and vibrations during intermodal transit (sea, rail, road). DN80 integrated butterfly and welded ball valves feature reinforced flanged interfaces and high-density PE-HD or passivated 316L stainless steel bodies to absorb multi-directional impact torque without stress cracking.
Modern DN80 valves incorporate precision-machined PTFE or FKM fluoropolymer seal seats that eliminate fluid entrapment pockets. This design prevents chemical crystallization, cross-contamination between reuse cycles, and micro-bacterial growth in sanitary applications like pharmaceutical intermediates and liquid food additives.
| Performance Benchmark Metric | Standard DN50 Valve (2-Inch) | Heavy-Duty DN80 Valve (3-Inch) | Engineering Operational Impact |
|---|---|---|---|
| Bore Nominal Diameter | 50 mm (1.97 in) | 80 mm (3.15 in) | +60% internal diameter expansion |
| Flow Coefficient (Kv / Cv Factor) | ~ 65 m³/h | ~ 185 m³/h | +184% volumetric throughput capacity |
| Discharge Time (1000L Water @ 1 bar) | approx. 3.5 - 4.2 minutes | approx. 1.2 - 1.5 minutes | Saves 2.5+ minutes per container discharge |
| Viscous Media Handling (> 5,000 cPs) | High pressure drop, prone to clogging | Smooth laminar flow, low fluid shear friction | Ideal for paints, polymers, molasses & resins |
| Standard Outlet Thread Interface | S60x6 Coarse Thread | S100x8 Coarse Thread / Camlock / BSP | Robust thread engagement resisting cross-threading |
Why Top Global Procurement Teams Source DN80 Valves from China
China's chemical container components industry has evolved from low-cost manufacturing into a high-precision, vertically integrated OEM/ODM power center. Here is how our manufacturing ecosystem delivers unmatched technical and commercial advantages.
From virgin High-Density Polyethylene (HDPE 5502BN grade) resin synthesis to high-precision investment casting of 304 and 316L stainless steel, leading Chinese suppliers maintain complete vertical control. We verify melt flow index (MFI), tensility, and chemical purity at the raw material stage, guaranteeing zero recycled contaminants in critical chemical sealing parts.
Our factories utilize multi-axis CNC machining centers, high-tonnage robotic plastic injection presses (800T to 1600T), and ultrasonic welding stations. Every DN80 valve stem, flap disk, dynamic seal gasket, and securing nut is manufactured to precise engineering tolerances, eliminating manual alignment errors and operational binding.
To ensure zero defect rates under rigorous freight conditions, every DN80 valve lot undergoes hydrostatic pressure testing (up to 2.5 bar), dry air pneumatic pressure decay tests (0.2 bar for 60 seconds), mechanical handle cycle durability tests (> 3,000 open-close actuations), and chemical exposure seal swelling tests.
Whether your fleet requires custom color-coded handles for hazmat visual identification, specialized company branding molded into the valve body, non-standard thread pitches (e.g., S100x8 to Camlock adapters), or custom seal compounds (EPR, NBR, Viton, EPDM), Chinese manufacturers offer rapid prototyping and low-cost mold development turnaround.
DN80 Valve Architectural Selection & Material Compatibility
Choosing the optimal DN80 IBC valve requires matching chemical characteristics, operating temperatures, and mechanical handling demands with the appropriate body geometry and elastomeric sealing compounds.
Primary Materials: Blow-molded HDPE body with PE/PTFE valve disk.
Best For: General chemical liquids, water treatment, agricultural fertilizers, neutral detergents, and high-volume industrial fluids. Compact profile, lightweight, cost-effective, and fully recyclable alongside standard HDPE IBC bottles.
Primary Materials: Investment Cast SS304/SS316 stainless steel with solid PTFE seats.
Best For: Aggressive organic solvents, concentrated acids, aromatic hydrocarbons, high-temperature liquids (> 80°C), and hazardous UN dangerous goods where maximum shear strength and zero permeability are mandatory.
Primary Materials: FDA-compliant Polypropylene or passivated SS316 with White EPDM/Silicone gaskets.
Best For: Liquid food processing, concentrated juices, edible oils, cosmetics, and pharmaceutical intermediates requiring quick-connect hose coupling and CIP (Clean-in-Place) sterilization protocols.
Polymer Sealing & Chemical Resistance Matrix
| Seal Compound Type | Operating Temp Range | Chemical Resistance Strengths | Media Limitations (Avoid Usage) |
|---|---|---|---|
| PTFE (Teflon / Fluoropolymer) | -40°C to +180°C | Universal chemical inertia, concentrated acids, aggressive solvents, strong alkalis | Fluorinated gases under high pressures and molten alkali metals |
| EPDM (Ethylene Propylene) | -30°C to +130°C | Steam, hot water, brake fluids, diluted acids, ketones, alcohols | Petroleum oils, mineral oils, aromatic hydrocarbons, gasoline |
| FKM / Viton (Fluoroelastomer) | -15°C to +200°C | Petroleum derivatives, aromatic hydrocarbons, mineral acids, oils, fuel oil | Low molecular weight organic acids (formic, acetic), hot water/steam |
| NBR (Nitrile Rubber) | -20°C to +100°C | Hydraulic oils, animal fats, vegetable oils, aliphatic hydrocarbons, water | Polar solvents (MEK, acetone), ozone, chlorinated hydrocarbons |
Localized Application Scenarios & Enterprise Bulk Solutions
DN80 IBC valves play a critical role across diverse global market sectors. Our specialized manufacturing caters directly to industrial supply chain challenges worldwide.
High-viscosity pesticide formulations, liquid fertilizers, and herbicide concentrates contain surfactants that easily degrade standard seals. Our DN80 integrated butterfly valves with modified fluoropolymer gaskets prevent valve binding, guarantee hermetic closure during seasonal outdoor storage, and facilitate rapid discharge into crop-sprayer aircraft or tractor tanks.
During long-distance intermodal transport, temperature fluctuations induce pressure changes inside IBC totes. DN80 welded ball valves featuring integrated pressure relief caps prevent container ballooning or wall collapse, while heavy-duty SS316 bodies provide absolute security against fire hazards and static electrical discharge in refinery zones.
High-fructose corn syrup, liquid sugar, wine, dairy concentrates, and edible oils require high-flow DN80 valves compliant with EU 10/2011 and US FDA sanitary specifications. Smooth internal bore geometry eliminates internal stagnant zones, ensuring complete product evacuation without leaving costly residue behind inside the container liner.
Tote reconditioners and industrial recyclers require replacement DN80 valves that thread effortlessly onto diverse blow-molded bottles (including Schulte, Mauser, and Greif styles). Our universal thread adapter profiles allow fast refurbishment, enabling sustainable circular economy practices for hazardous liquid waste collection.
Global B2B Procurement Risk Mitigation & Inspection Protocol
To protect your operations against unexpected downtime, structural failures, or environmental spills, implement this engineering verification checklist when selecting a China DN80 IBC valve supplier.
Request factory hydrostatic burst pressure test reports. Standard operational ratings should handle continuous working pressures of 1.5 bar to 2.5 bar, with instantaneous burst tolerances exceeding 5.0 bar to survive dynamic transit shocks.
If transporting hazardous materials (UN Packaging Groups II and III), verify that the valve assembly holds official UN certification marks (UN 31HA1/Y design approval) issued by recognized international inspection agencies.
Ensure the valve inlet nut matches your container neck specification (e.g., standard S100x8 male/female buttress thread pitch) and that the outlet features a reliable dust cap and safety sealing foil pin.
Future Industry Trends: Smart Packaging & Eco-Engineering
The industrial packaging sector is undergoing rapid technology transitions driven by ESG decarbonization mandates and Digital Supply Chain integration.
Traditional valves containing mixed metallic springs or incompatible polymer handles complicate end-of-life recycling. Next-generation DN80 valves utilize 100% all-polyolefin construction (HDPE body, PE disk, PE handle), allowing the entire tote container and valve assembly to be ground into pure PCR resin without manual disassembly.
Leading Chinese OEM manufacturers are embedding passive RFID microchips and tamper-evident electronic seals into the DN80 valve handle casing. This enables automated batch tracking, tamper logging, digital seal verification, and real-time inventory monitoring across global warehouse networks.
Tightening environmental laws regarding Volatile Organic Compounds (VOCs) require zero atmospheric leakage. Advanced multi-lip stem seals and live-loaded spring packing prevent micro-evaporation of volatile solvents through the valve actuating stem under ambient thermal spikes.
Frequently Asked Questions (Technical & Commercial FAQ)
Detailed answers provided by our senior engineering team to assist international buyers, packaging engineers, and supply chain managers.
Complete IBC Containers, Parts & Pallet Accessories
Explore our full line of industrial bulk storage solutions, heavy-duty replacement components, and structural container reinforcements.